
- All
- Product Name
- Product Keyword
- Product Model
- Product Summary
- Product Description
- Multi Field Search
 English




| Quantity: | |
|---|---|


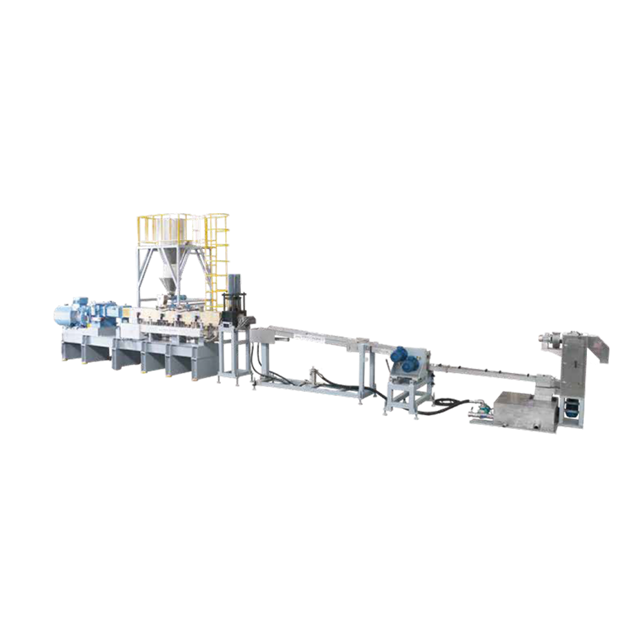
The CJWH PET Twin-Screw Pelletizing Line processes prepared material through extrusion and pellet formation. The model table lists an L/D range of 40-48 and speeds of 300-500 rpm.
The twin-screw route should be evaluated around the intended PET material and the pellet properties required for reuse. Screw structure is one part of that decision, while feed preparation, filtration and downstream handling remain separate scope questions. The three listed configurations provide screw, motor, L/D, speed and output data for comparison. Buyers should use the model-specific table rather than unrelated generic capacity statements. The line also needs a clearly selected cooling and cutting arrangement so the proposal describes the full route to collected pellets. PET origin, moisture and contamination should accompany the capacity request, particularly when comparing clean production material with recovered feed. A packaging application does not establish food-contact approval; the final acceptance requirements must follow the customer's own intended manufacturing use.
CJWH PET Twin Screw Pelletizing Line
Define the PET source, preparation and intended pellet use at the start of the project. Record moisture and contamination conditions. The required material quality should guide the process discussion rather than using general plastics applications to broaden the specification.
PET origin helps define the preparation discussion. Identify production scrap or recovered feed and describe treatment already completed. The proposed line should be reviewed against that actual entry condition, with the intended pellet application providing direction for quality requirements and any additional preparation scope.
The twin-screw arrangement supports mixing and melting during material processing. Barrel heating control is described for the extrusion system. Review the chosen screw and temperature configuration around the actual PET feed and desired pellet condition.
Twin-screw processing describes the extrusion structure, while the complete recycling duty includes material preparation and pellet handling. Compare the proposed configuration with the feed and output requirements. The structure should not be treated as evidence that upstream washing or application-specific quality checks are unnecessary.
CJWH75 lists 500-600 kg/h and CJWH85 lists 600-800 kg/h. The third row, identified as CJWS95, lists 1000-1500 kg/h. Keep that published identifier until the exact supplied model designation is confirmed.
The output bands belong to the listed configurations. Review them with screw and motor data on a consistent feed basis. Generic capacity text should not replace those rows, and a selection should explain the intended PET condition rather than treating catalogue output as universally available.
Model | L/D | Speed(rpm) | Capacity KG/H |
CJWH75 | 40-48 | 300-500 | 500-600 |
CJWH85 | 40-48 | 300-500 | 600-800 |
CJWS95 | 40-48 | 300-500 | 1000-1500 |
All three rows list 40-48 L/D and 300-500 rpm. These ranges help compare the extrusion configuration. They do not establish one universal operating point or the same production output across all listed models.
L/D and speed ranges are configuration information, not a single operating recipe. Their selection should accompany screw and motor review for the intended material. Confirm the supplied arrangement and proposed operating basis so the buyer can distinguish available options from the configuration described in the quotation.
Filtration is described as part of the process. Agree the number and type of screen changers and the relevant contamination duty in the proposal. The twin-screw name does not establish a separate second extruder or a guaranteed purity level.
Filtration needs a defined scope at the intended process positions. Descriptions of main and auxiliary filtration do not alone establish how many extruders will be supplied. Request a clear equipment sequence and selected filter arrangement rather than inferring the complete structure from a broad process phrase.
The product description identifies cooling and pelletizing functions, with vibration screening for pellet handling. Set the pellet requirements and collection arrangement. Confirm the selected downstream equipment so extrusion capacity and pellet handling can be assessed together.
Cooling, cutting and collection complete the route from extrusion to usable pellets. The proposal should name the selected method and identify the equipment associated with it. Keeping these items visible helps buyers compare complete lines with the same output boundary instead of extruder specifications alone.
The JWT PET single-screw line offers a different extrusion route. The PET bottle washing line addresses upstream recovered-bottle preparation. Select a coordinated process rather than treating washing and pelletizing as interchangeable functions.
The alternatives address different process decisions: washing prepares material, while another extrusion structure offers a separate pelletizing route. Review both with the same feed and application requirements. This makes the comparison relevant to the actual recovery task and avoids assuming that one stage replaces another.
Submit feed origin, preparation details, target output and pellet application to DYUN's PET extrusion team. Ask for the exact model identifier and filtration arrangement. Include the required operating and quality targets in the technical discussion.
Include sample condition, intended pellet properties and the proposed output basis in the enquiry. Add existing preparation equipment and the scope needed after extrusion. These details allow the supplier to identify the selected configuration and explain its interfaces within a complete PET-recycling installation.
The DYUN corporate introduction provides context for its recycling machinery operations. A PET twin-screw project should establish the precise model identity and align extrusion, filtration and pellet handling with the prepared feed.
The manufacturer discussion should connect PET preparation with the selected extrusion and pellet-handling route. A complete proposal identifies filtration and cutting scope and preserves the exact selected configuration data. This provides a clearer basis for purchase review than a general twin-screw description or packaging application claim.
 JWELL factory scene displayed on DYUN's company page.
Start with PET origin, preparation condition and required pellet properties. Compare screw, motor, L/D and output data together, then define filtration and pellet handling. The extrusion structure alone does not describe the full recovery route.
The model-specific bands are 500–600, 600–800 and 1000–1500 kg/h. Use those rows for initial comparison and assess the intended feed. They take priority over unrelated generic capacity descriptions elsewhere in the source material.
The table gives 300–500 rpm and an L/D range of 40–48. These are selection entries rather than one fixed operating recipe. Confirm the selected screw, motor and process configuration for the intended PET material.
No. A potential packaging use does not establish food-contact or other application approval. Preparation requirements, pellet checks and any required compliance evidence must be assessed separately for the customer's intended use.
It should identify the selected extrusion configuration, filtration, cooling, cutting and collection equipment. Provide representative PET and the required pellet output. Separate existing preparation equipment from new supply so quotations describe comparable process boundaries.
Confirm the exact selected label and dimensional data in the technical proposal; one source row uses a different series prefix. Also review motor selection, filtration scope and installation requirements. The ordering specification should follow confirmed equipment data rather than an assumed naming pattern.


